Large shafts and gear shafts
Stepped shafts · gear shafts · spindles
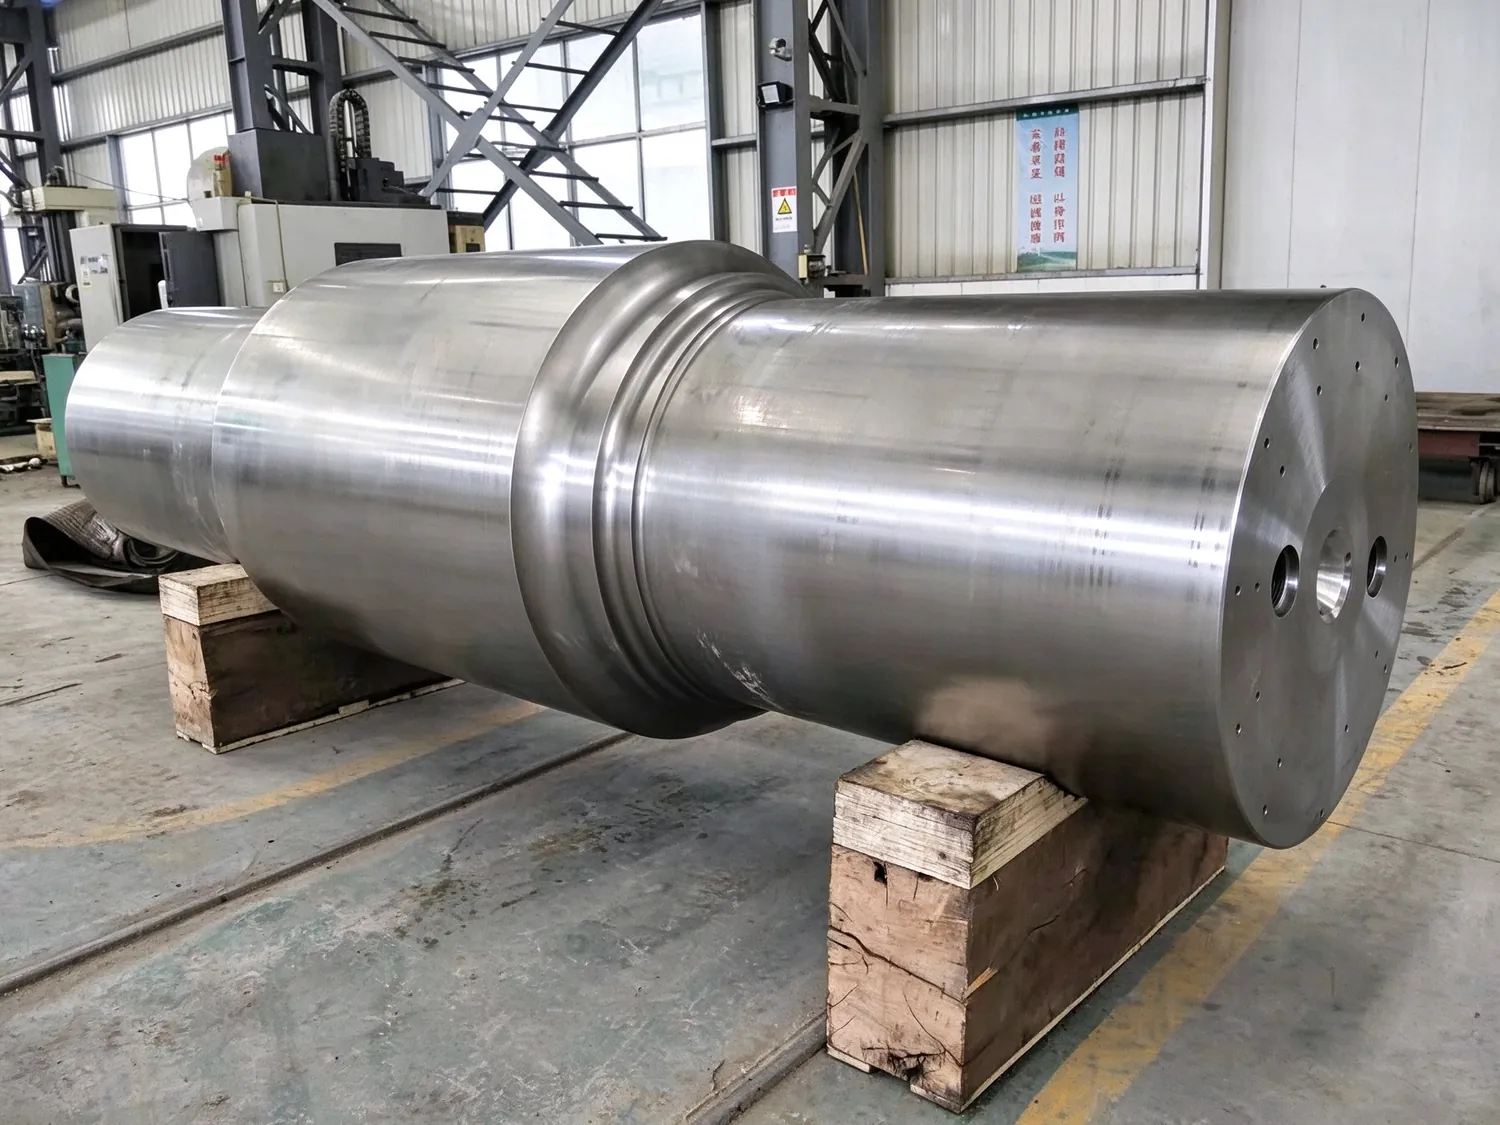
Stepped shafts, gear shafts and spindles. Long parts distort before they lose accuracy, so the order is fixed: rough turn, quench and temper, finish turn on a steady rest, then grind the bearing and seal seats last. Gear shafts add hobbing and induction hardening to the same route, so the journals and the teeth are referenced to one another.
Specifications
- Turning
- 5 m horizontal lathe · CNC vertical lathe
- Features
- Keyways · splines · threads · drilled flanges
- Heat treatment
- Quenching and tempering · induction hardening
- Inspection
- UT · hardness · radial runout
Typical use
- Mill and crusher main shafts
- Gear shafts for reducers
- Pump and fan shafts
- Spindles and drive shafts for heavy equipment
If a shaft needs a heat-treat step your drawing does not call for, we raise it at review — changing the sequence after roughing is what makes long parts move.
Typical process
01
Cutting and forging
material selected by grain direction
02
Rough turning
stepped stock removal
03
Quenching and tempering
less distortion later
04
Finish turning
steady rest, follow the cut
05
Keyways / drilling
position per drawing
06
Grinding
bearing and seal seats
07
UT and inspection
UT · hardness · runout
08
Coating and dispatch
rust prevention and lifting protection
Housings · hubs · bearing seats · machined blanks
Need us to confirm fixturing and operations against your drawing? Send the part size, material and quantity; we will review the process against the machines we have.
Send a drawing, get a quote