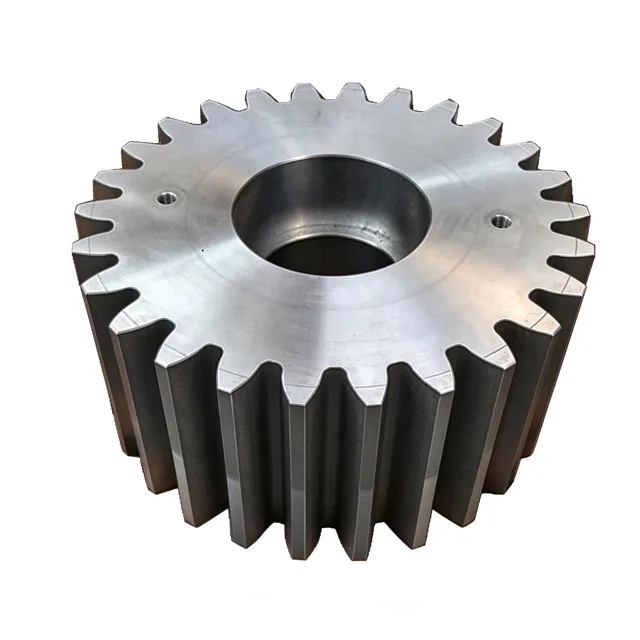
Gears & PinionsSpur gears
Hardened Helical Cylindrical Gear
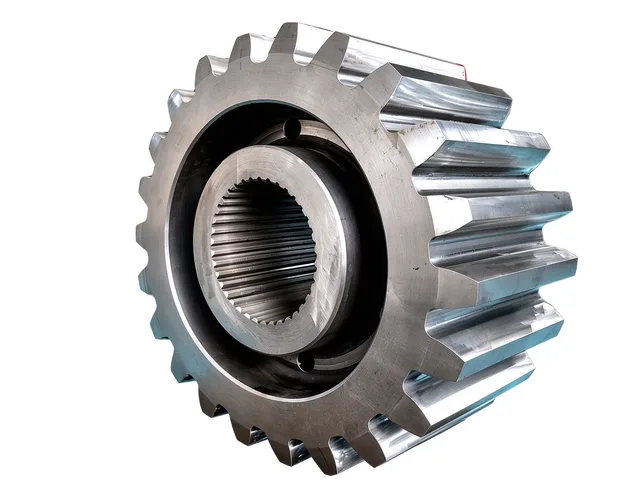
Hardened helical cylindrical gear with an integral hub, precision centre bore and radial oil holes, used as the driven wheel in gearboxes for speed reduction and torque multiplication.
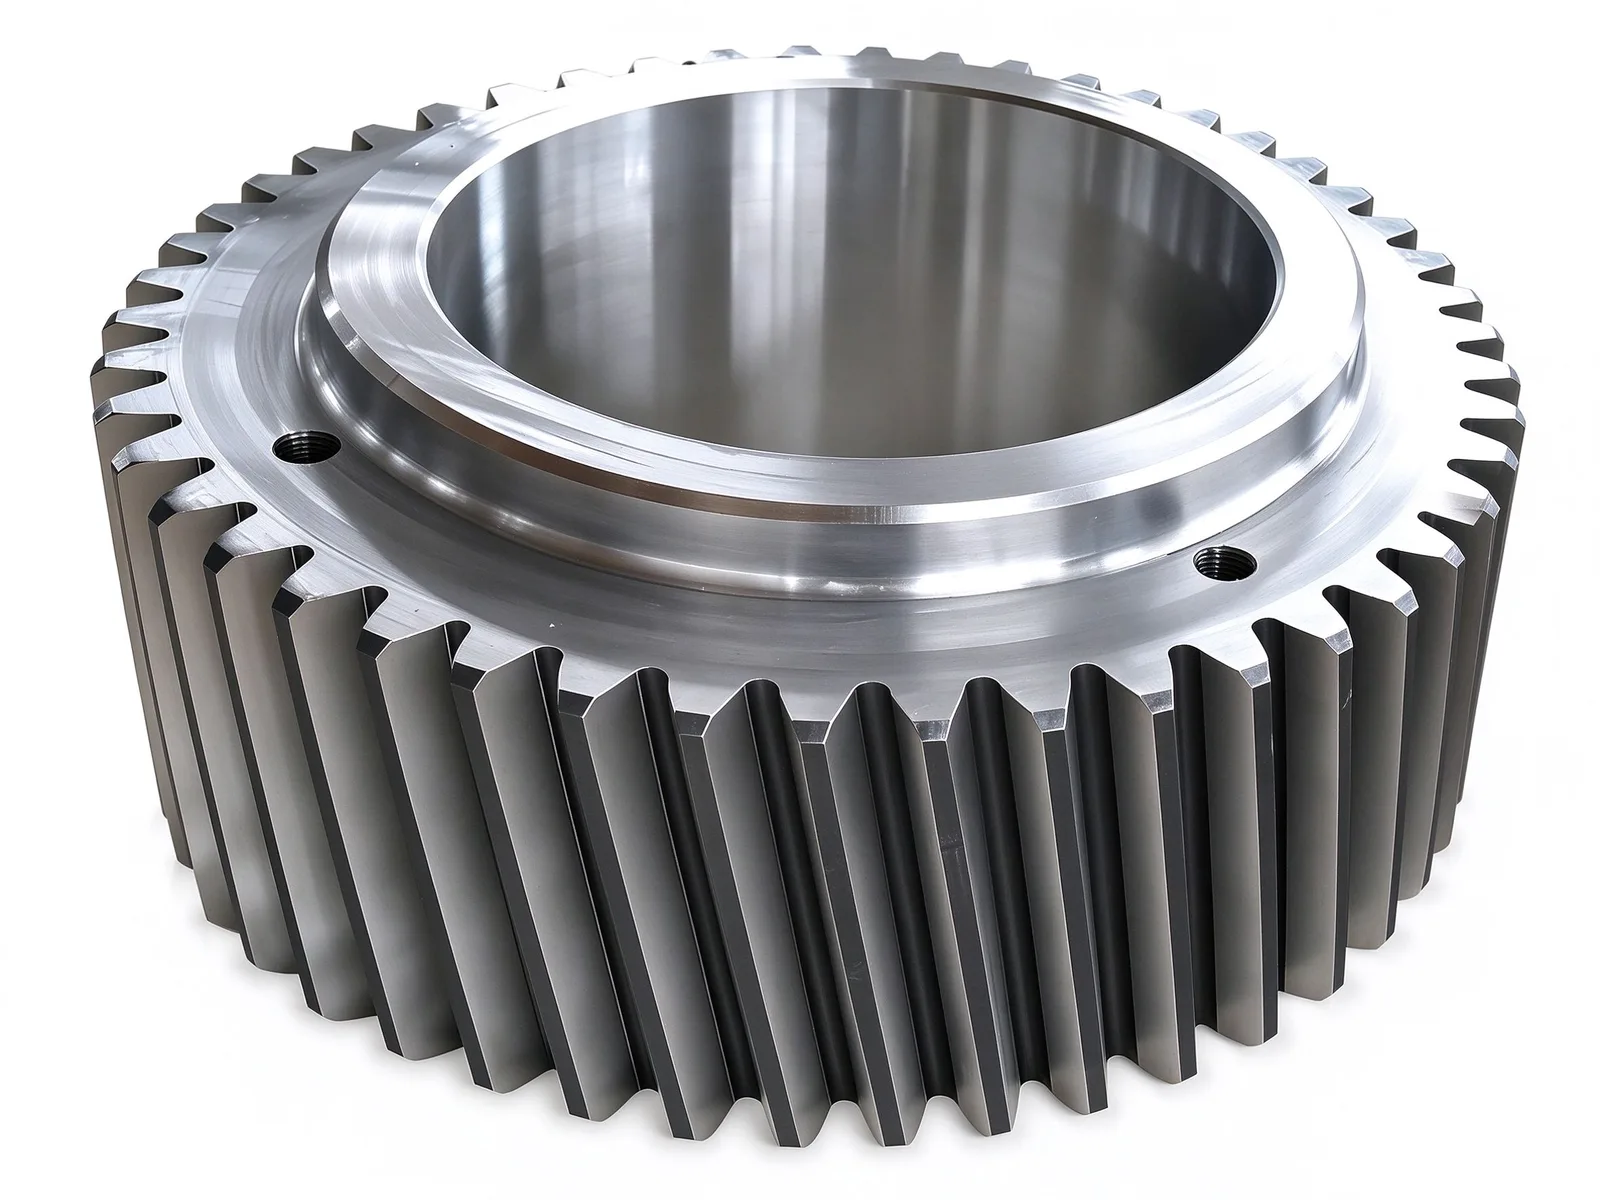
Tooth design and transmission behaviour
Helical cylindrical teeth give a higher contact ratio than straight teeth, so the gear runs more smoothly and quietly and suits continuous medium-to-high speed, high-torque duty. Tooth flanks are ground, keeping profile accuracy and surface finish within hardened-gear requirements.
Running as the driven wheel against a pinion shaft, it reduces speed and multiplies torque; the hardened flank layer with a tough core withstands alternating shock loads.
Hub structure and mounting
The precision-machined centre bore takes the shaft through an interference fit or a keyed connection to transmit torque, while the thickened hub raises overall rigidity and limits distortion under high torque.
Radial threaded holes on the hub face serve as lubrication ports feeding the fit surface, and as jacking holes during disassembly for easier maintenance.
Material and heat treatment
Forged blanks in alloy structural steels such as 20CrMnTi and 42CrMo are carburized and quenched, or quenched and tempered with induction-hardened tooth flanks, balancing wear resistance at the surface with toughness in the core.
Blanks can also be supplied as castings or rolled rings. Tooth pitch, runout, hardness and ultrasonic testing are checked in-house, with dimensional and geometric re-inspection after heat treatment.
Customisation and lead time
Outside diameter, tooth count, module, helix angle, bore and keyway are made to drawing; maximum outside diameter Ø10 000 mm and module up to M60, with straight, helical, herringbone and internal tooth forms available.
Typical materials are 45#, 42CrMo and ZG270-500; heat treatment covers quenching and tempering and high-frequency flank hardening up to Ø10 000 mm. Typical lead time is within 90 days.
Specifications
- Material
- 20CrMnTi / 42CrMo
- Tooth type
- Helical cylindrical teeth
- Heat treatment
- Carburizing and quenching; or quenching and tempering + induction hardening of tooth flanks
- Structure
- Integral hub with precision centre bore
- Hub oil holes
- Radial threaded holes, for lubrication and disassembly
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part