Shafts & RollersRolls
High-Pressure Grinding Roll Assembly
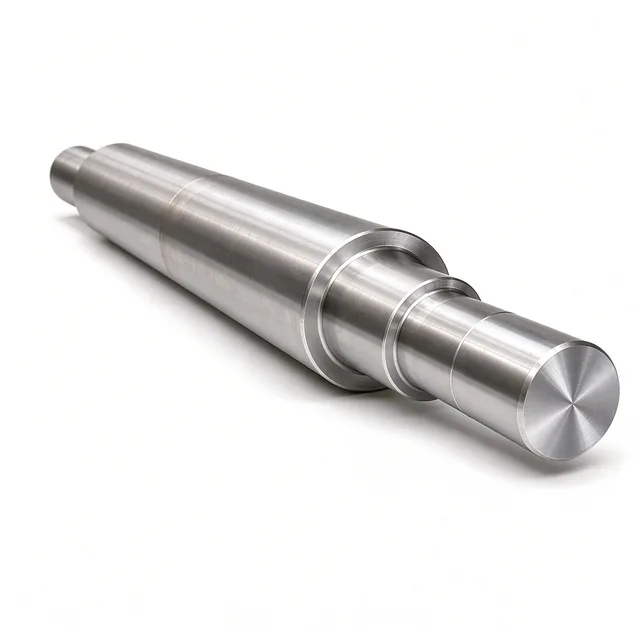
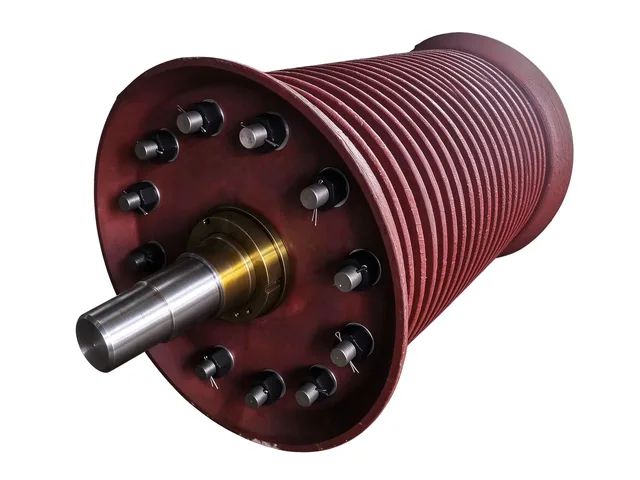
Roll assembly for high-pressure grinding mills: a hardfaced wear layer on the roll body and precision-machined stepped journals, rebuildable by re-welding for cement and mining comminution.
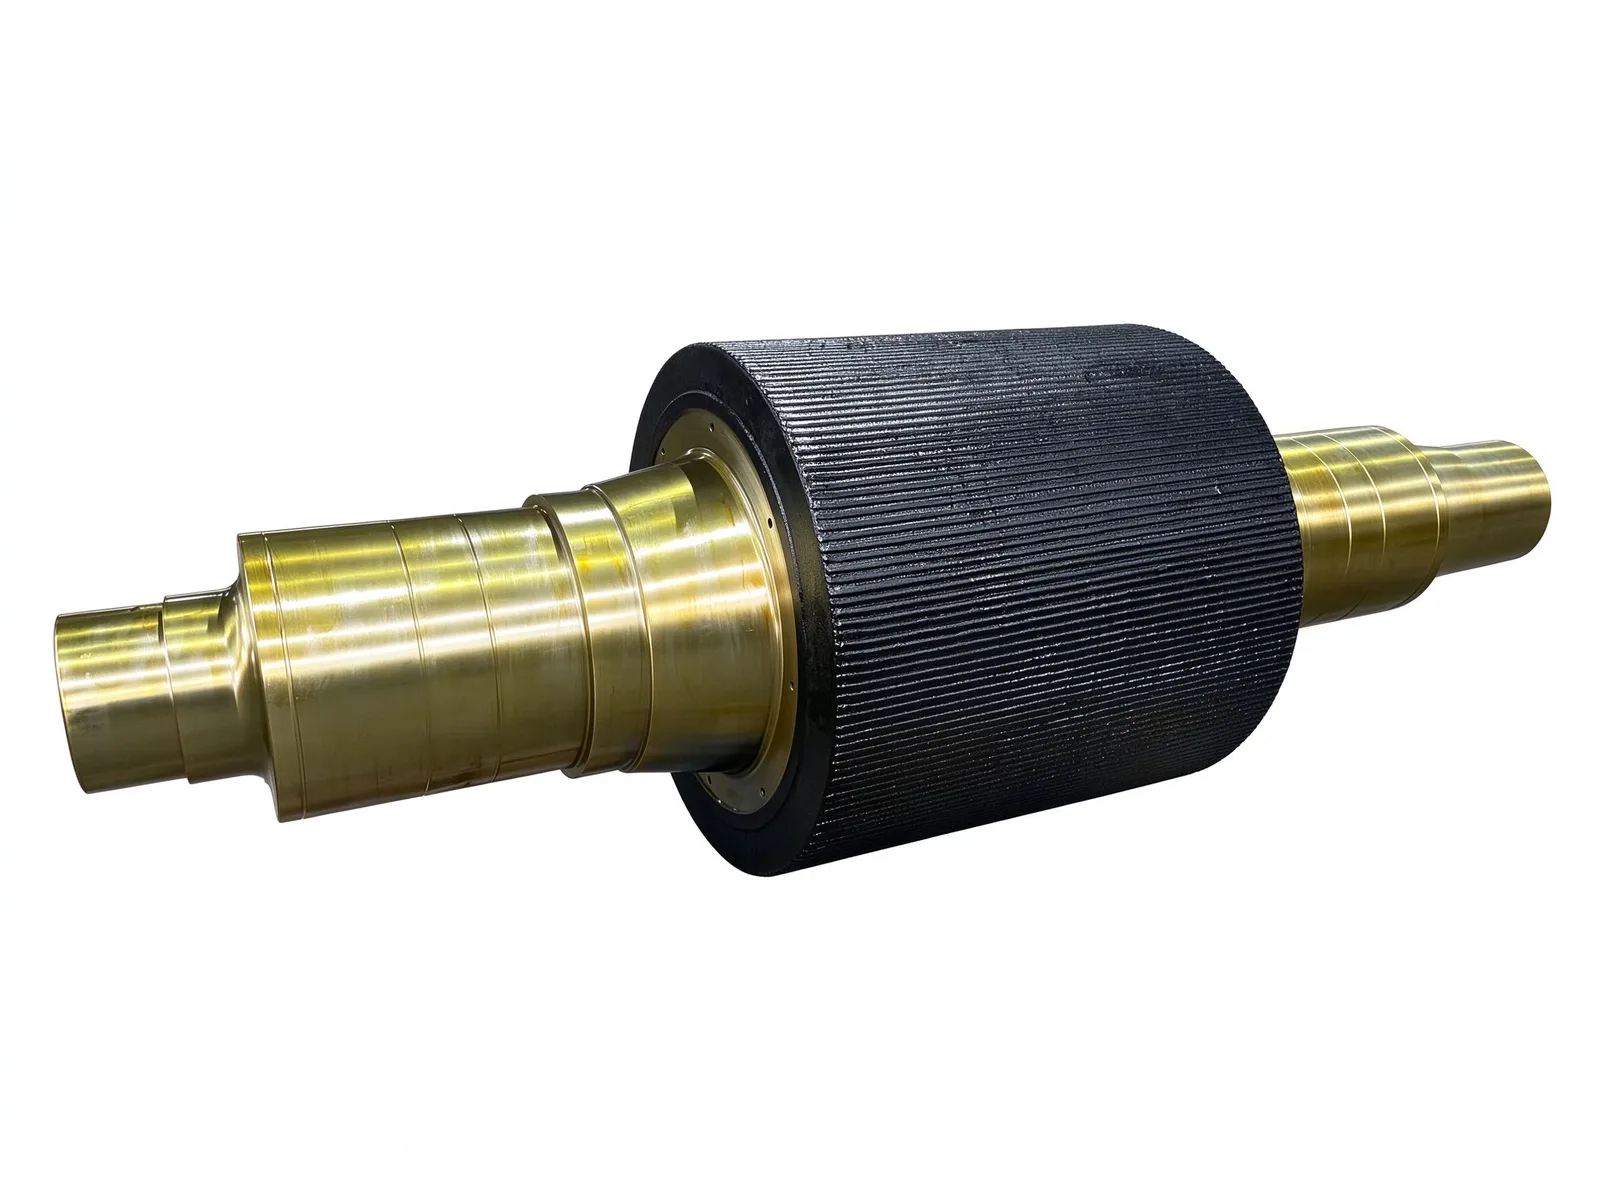
Roll body and wear layer
The working surface is a hardfacing layer built up bead by bead over the roll body; the fine circumferential weld ridges raise the bite friction so the material bed is drawn into the gap instead of slipping. This layer takes the direct impact and abrasive wear of the crushing zone, and once it is worn it can be rebuilt by re-welding on the original body rather than replacing the whole part, which keeps long-term maintenance cost down.
Machining capability
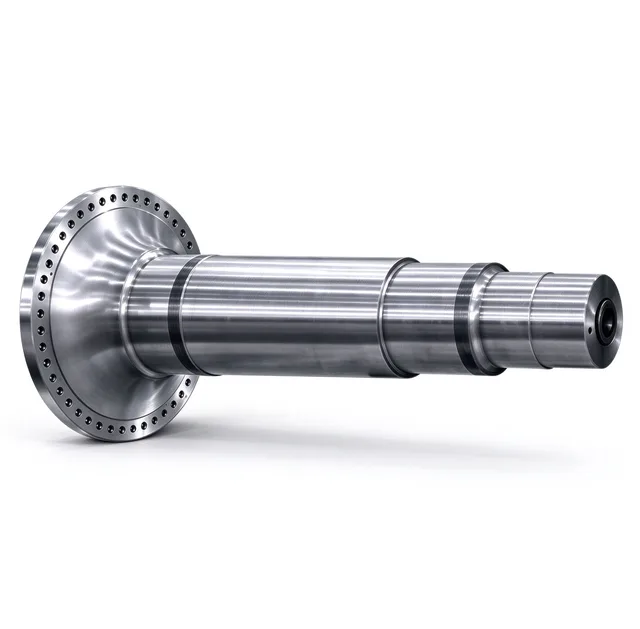
Rolls are turned, ground and hardfaced in-house. Maximum machinable length is 10 000 mm including clamping and maximum diameter Ø1 500 mm, with journal tolerance h6 / IT7 and radial runout ≤0.02 mm. Keyways, splines, threads and end-face flange holes can be cut in the same process route, and the stepped journals are machined to locate bearings and seals precisely under heavy radial load and torque transmission.
Where it is used
The assembly usually runs in pairs, a fixed roll and a movable roll turning toward each other, crushing the material bed by high-pressure inter-particle compression. It is commonly used in cement raw meal and clinker pre-grinding, in iron ore and non-ferrous ore secondary crushing, and in the pre-treatment of slag and steelmaking waste.
Quality control and customization
Journals are measured one by one for diameter and runout, and the roll body is checked for straightness and surface condition before assembly. Roll geometry, wear layer thickness, bearing seat fits and drive connections are made to the customer's drawing, with a typical lead time of 60 days.
Specifications
- Max. machinable length
- 10 000 mm (including clamping)
- Max. diameter
- Ø1 500 mm
- Journal tolerance
- h6 / IT7
- Radial runout
- ≤0.02 mm
- Typical lead time
- 60 days
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part