ShaftsTransmission shafts
Jaw Crusher Eccentric Shaft
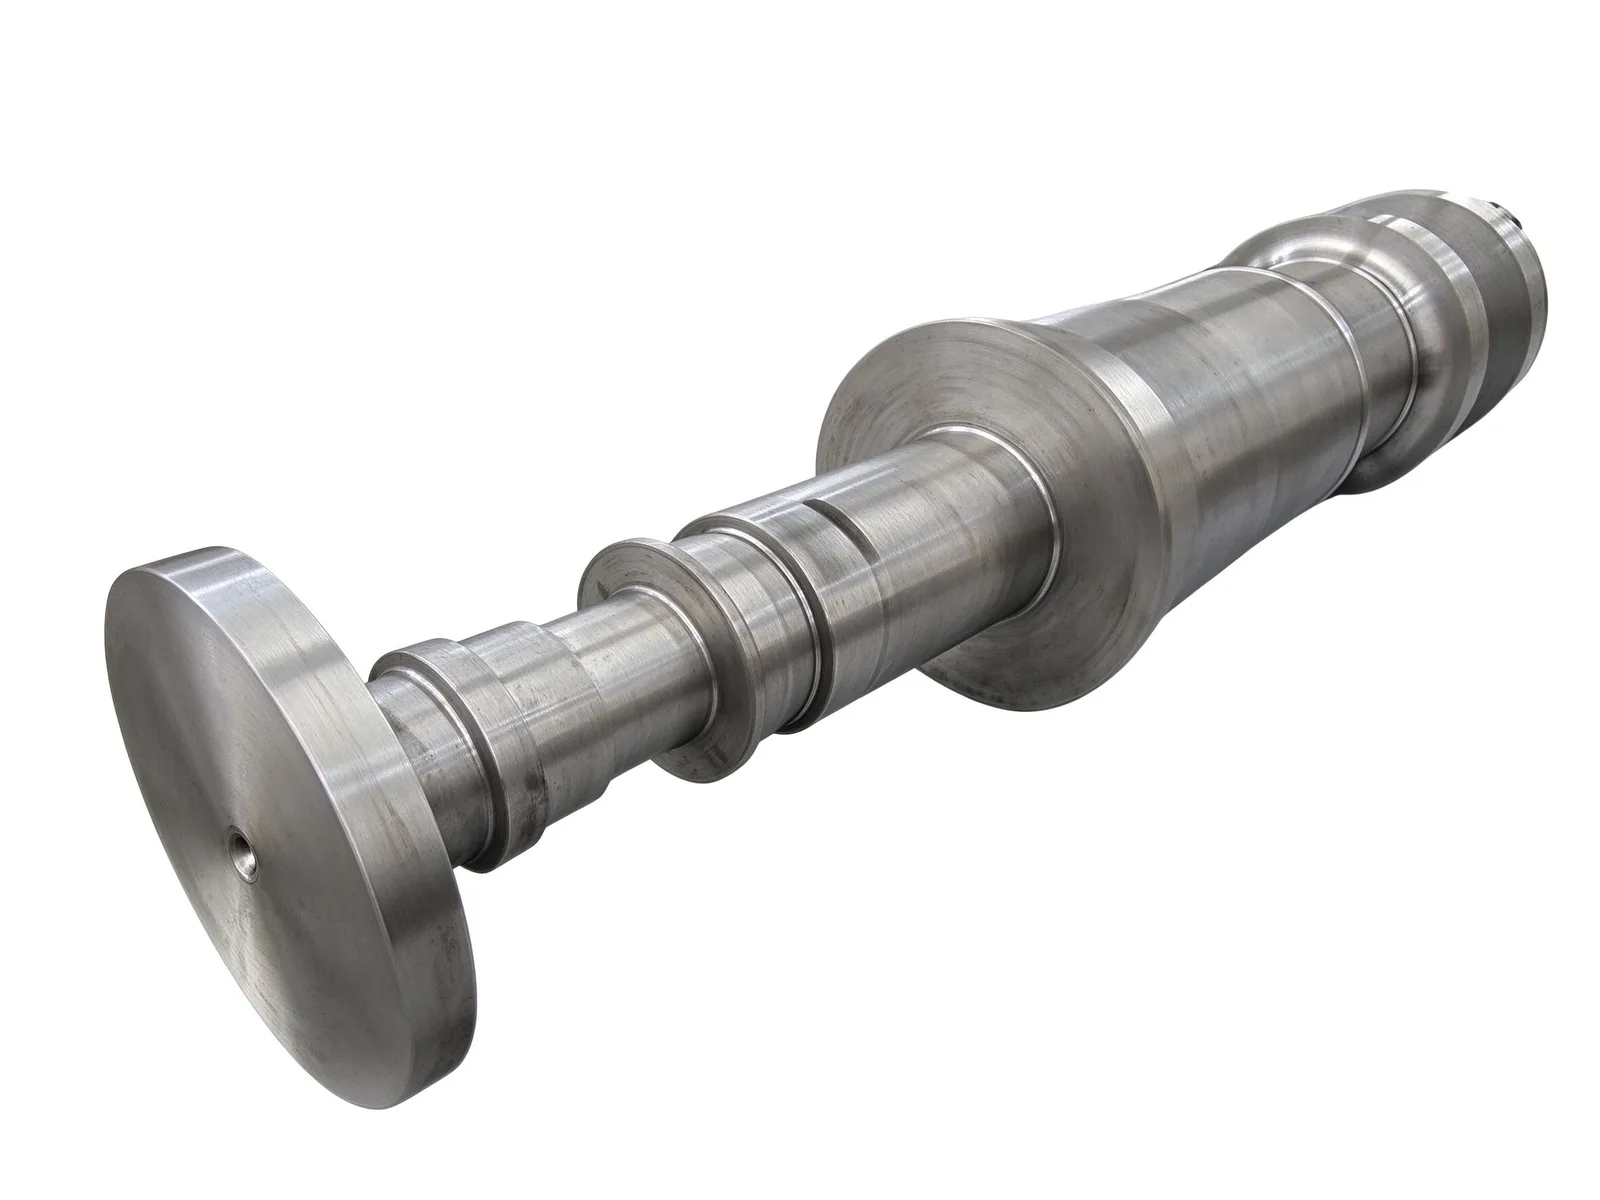
One-piece forged eccentric shaft for jaw crushers, with a gear input end, an eccentric journal that drives the swing jaw, and a flywheel mounting end.
Structure and Function
This is the eccentric main shaft of a jaw crusher. The right end takes power from the drive gear, the middle eccentric section converts rotation into the reciprocating swing of the movable jaw, and the left end carries the flywheel. The shaft is forged as one piece rather than assembled from separate sections, which keeps stiffness consistent along the full length under repeated impact.
The stepped profile, collars, and end flange are turned and then ground at the bearing and fit surfaces, so the shaft seats correctly in the frame bearings and holds its position under load.
Material and Heat Treatment
The shaft is typically made from 42CrMo or 35CrMo alloy structural steel, forged, then normalized, quenched and tempered, and surface hardened. This combination gives the body toughness against cyclic shock while the running surfaces resist wear.
Critical mating surfaces are precision ground after heat treatment to control form and position, which is what allows the shaft to carry heavy crushing loads over a long service life.
Machining Capability
Shafts are machined on our own turning and grinding equipment up to a maximum length of 10,000 mm including clamping and a maximum diameter of Ø1,500 mm, with a single-piece weight of up to 8 t. Journals can be held to h6 / IT7 with surface roughness Ra 0.8 and radial runout within 0.02 mm.
Keyways, splines, threads, and end-face flange holes are all machined in-house, and quench-and-temper plus induction hardening can cover the full 10,000 mm length.
Every shaft is produced to the customer's drawing; eccentric throw, gear parameters, journal diameters, and flywheel mounting dimensions are confirmed from the drawing or from measured samples before production.
Quality Control and Delivery
Dimensions, form and position tolerances, runout, and hardness are checked on the finished part, with ultrasonic or magnetic particle inspection available when the drawing calls for it. Inspection records travel with the shipment.
Typical lead time is 8 to 12 weeks depending on size and quantity. Tell us the crusher model or send a drawing and we will confirm the feasible dimensions, material, and heat treatment for your application.
Specifications
- Material (typical)
- 42CrMo / 35CrMo
- Construction
- One-piece forged
- Heat treatment
- Normalizing, quenching and tempering, surface hardening
- Mating surfaces
- Precision ground
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part