Gears & PinionsRing gears
Large Cast Girth Gear
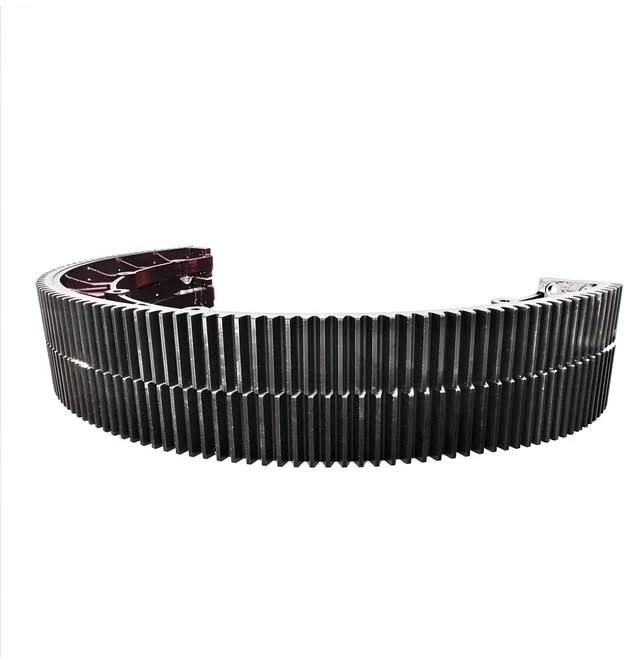
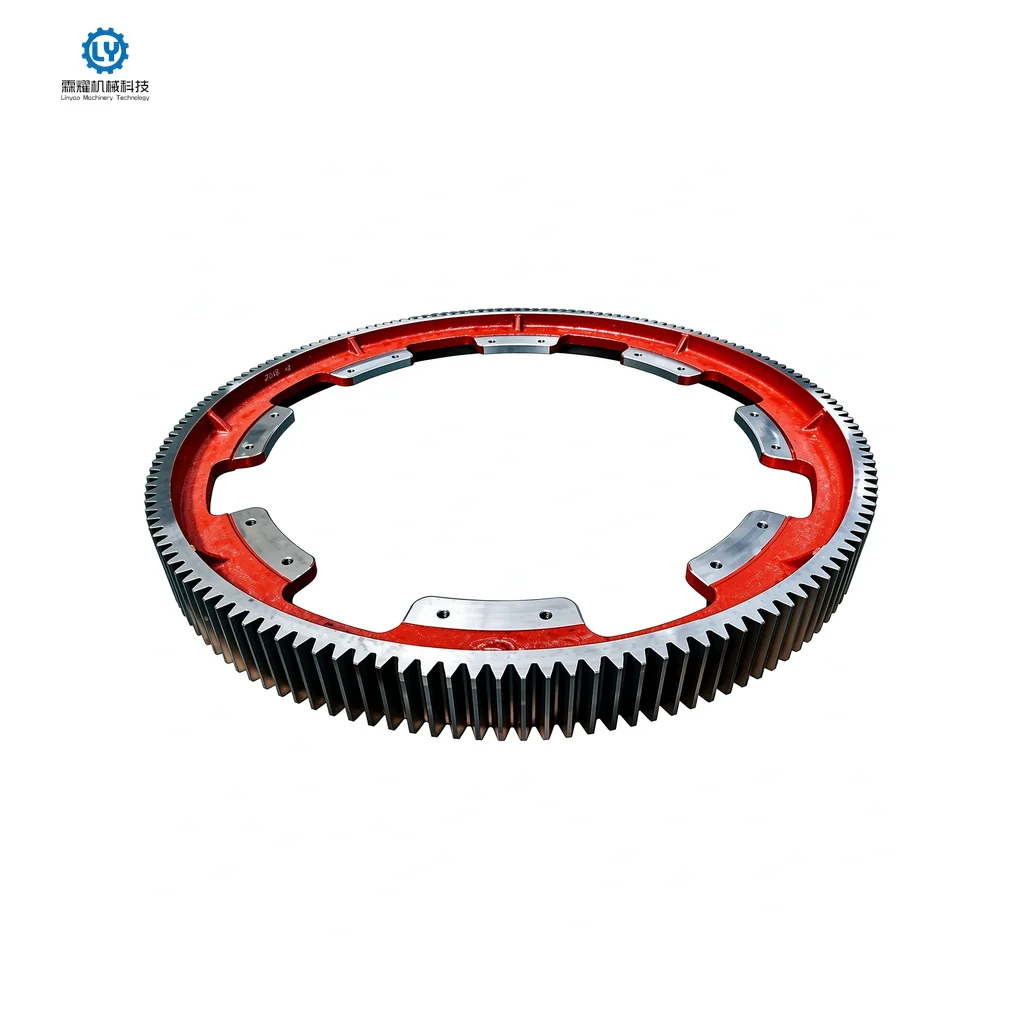
Segmented cast girth gear, bolted together on site, for heavy-duty shell drives such as rotary kilns and ball mills.
Machining Range
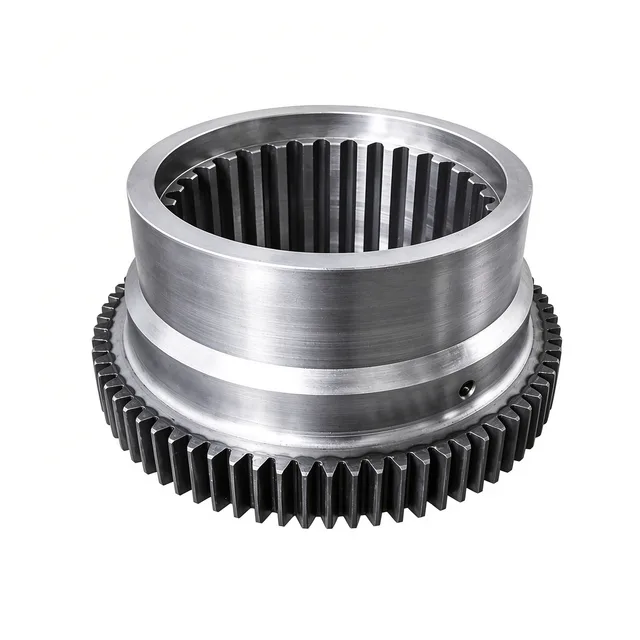
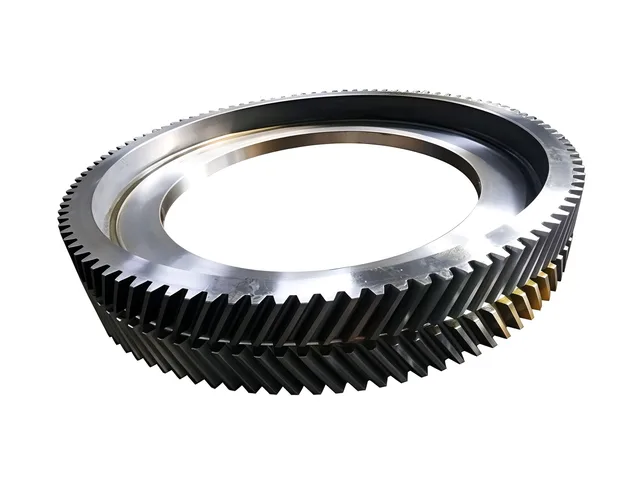
The girth gear is first cast, rough-turned and quenched and tempered, then finish-turned and gear-hobbed or gear-milled. External teeth can be straight, helical or herringbone; internal teeth and splines are also available. Maximum machinable outside diameter Ø10 000 mm, maximum module up to M60.
Segments are matched by number, trial-assembled and bolt holes fitted in-house; joint faces and pitch are aligned before shipment, shortening on-site assembly time.
Application Conditions
Mainly used for low-speed, heavy-load shell drives of rotary kilns, ball mills, rod mills and dryers in the cement, mining and metallurgy industries. The segmented structure keeps individual piece weight and dimensions within transport and lifting limits, while achieving diameters difficult to reach by integral casting.
Common materials are 45#, 42CrMo and ZG270-500; blanks can be castings, forgings or rolled rings, selected according to overall load and tooth surface stress.
Inspection and Lead Time
Pitch, runout, hardness and ultrasonic flaw detection are all self-inspected, with reports supplied with the parts. Heat treatment includes quenching and tempering and high-frequency tooth surface hardening, with maximum hardening diameter 10 000 mm.
Typical lead time within 90 days. Please provide drawings and module, number of teeth, pressure angle, material and mating pinion parameters for us to quote.
Specifications
- Structural Form
- Segmented, joint faces bolted together
- Process
- Casting, rough turning, quenching and tempering, finish turning, gear cutting
- Applicable Equipment
- Rotary kiln, ball mill, dryer
- Material Options
- 45#, 42CrMo, ZG270-500
- Customization
- Customized to drawing
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part