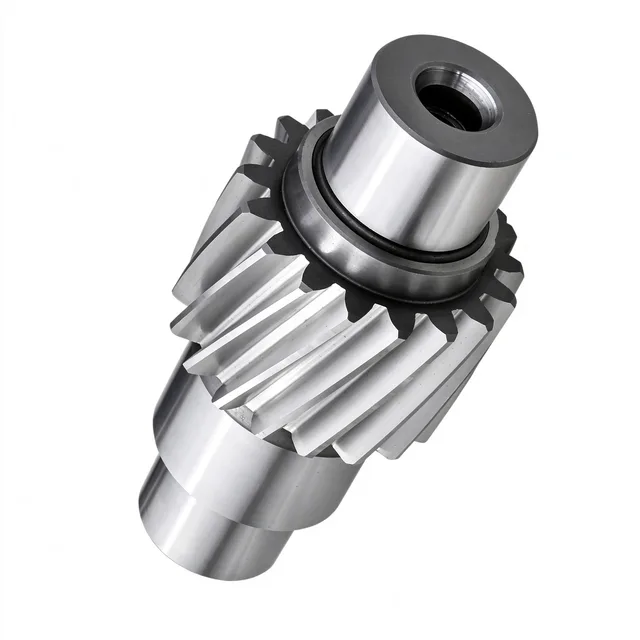
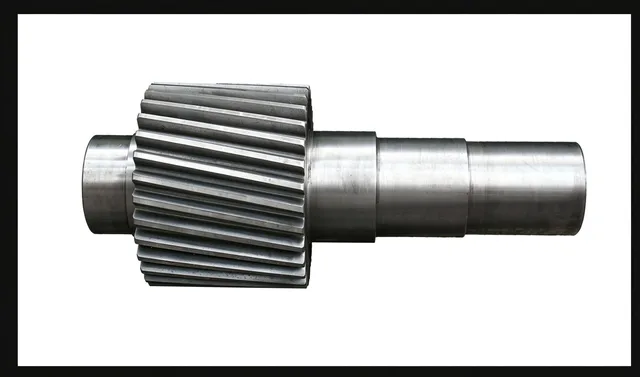
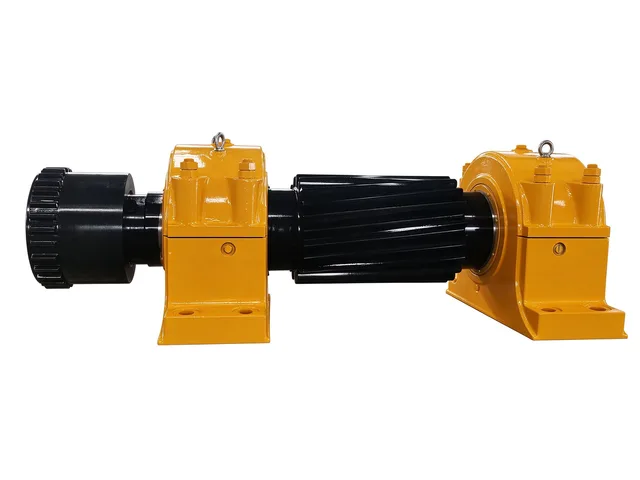
Gears & PinionsGear shafts
Heavy-Duty Large-Module Spur Gear Shaft
One-piece large-module straight spur pinion shaft for low-speed, heavy-load drives, with stepped bearing journals, keyway and center holes; custom-machined to drawing.
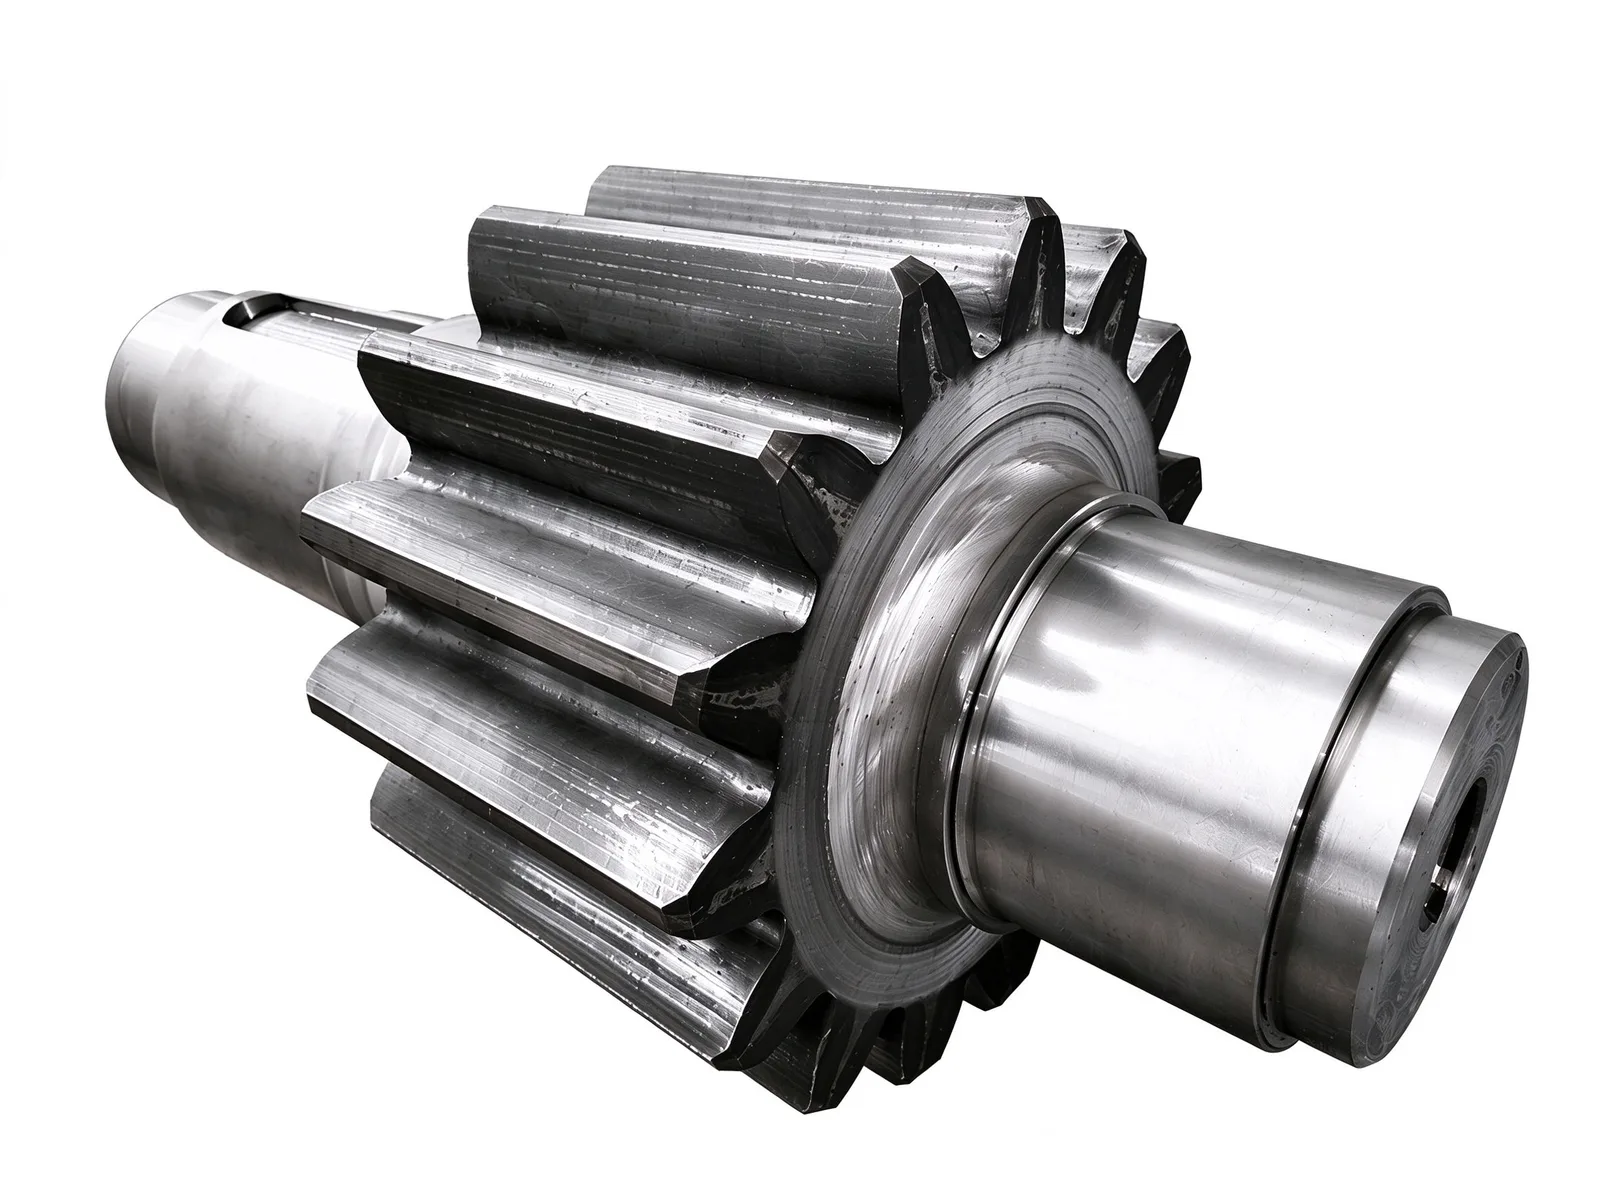
Integral Spur Gear Shaft Design
This is a one-piece large-module straight spur pinion shaft. The gear teeth and shaft body are made from a single blank, so there is no fitted joint between gear and shaft. Both ends are stepped support journals with locating shoulders; the left shaft end has a parallel keyway for power input, and the right end has a center hole for turning and grinding setup and for axial locking. The wide face and large module suit low-speed torque transmission. Final module, tooth count, pressure angle, face width, hardness and journal dimensions are confirmed from the drawing or measured sample.
Heavy-Duty Drive Applications
Straight spur teeth generate no additional axial force, which keeps bearing axial loads low and simplifies assembly and maintenance. The shaft is commonly used as the input pinion in heavy-duty industrial reducers, mine hoists, jaw and cone crushers, metallurgical mill drives, and large lifting and transport machinery. It is intended for low-speed, high-torque working conditions with shock loads; the exact duty rating depends on the confirmed gear parameters and mating gear.
Gear Cutting and Heat Treatment
For gear work in this category, the shop can cut outside diameters up to Ø10 000 mm and modules up to M60, covering straight, helical, herringbone and internal teeth; quenching is available up to 10 000 mm diameter. Typical materials include 42CrMo and 20CrMnTi, with 45# and ZG270-500 also available for gear blanks. Heat treatment can be quenching and tempering, carburizing and quenching, or tooth-surface induction hardening, followed by finish machining of the tooth flanks.
Inspection, Blanks and Custom Scope
Blanks can be supplied as castings, forgings or rolled rings, and ultrasonic testing is handled in-house. Inspection covers pitch, runout, hardness and ultrasonic testing as required, and dimensional and geometric reports can be provided. Custom options include tooth profile, module, face width, journal diameters, keyway and center-hole details, and heat treatment condition. Typical lead time for gear parts is within 90 days; final scope is set by the drawing and order quantity.
Specifications
- Typical material
- 42CrMo / 20CrMnTi
- Heat treatment
- Quenching and tempering or carburizing and quenching
- Tooth type
- Straight spur
- Construction
- Integral gear and shaft
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part