Gears & PinionsRing gears
Large Split Girth Gear for Rotary Kilns and Ball Mills
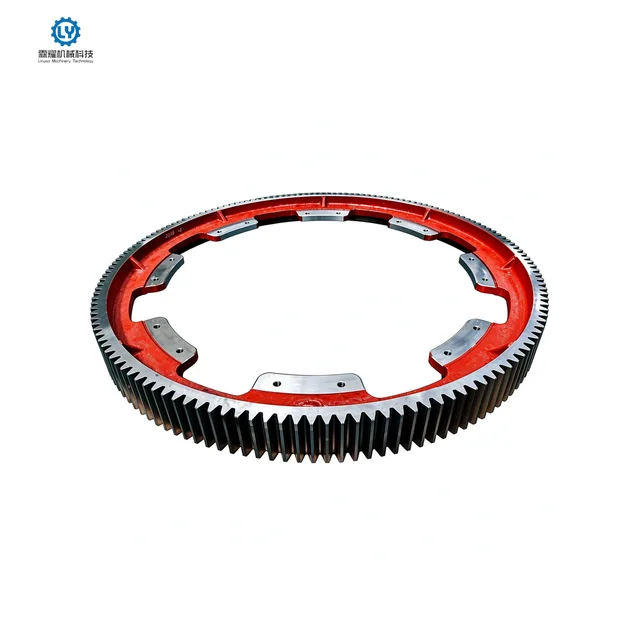
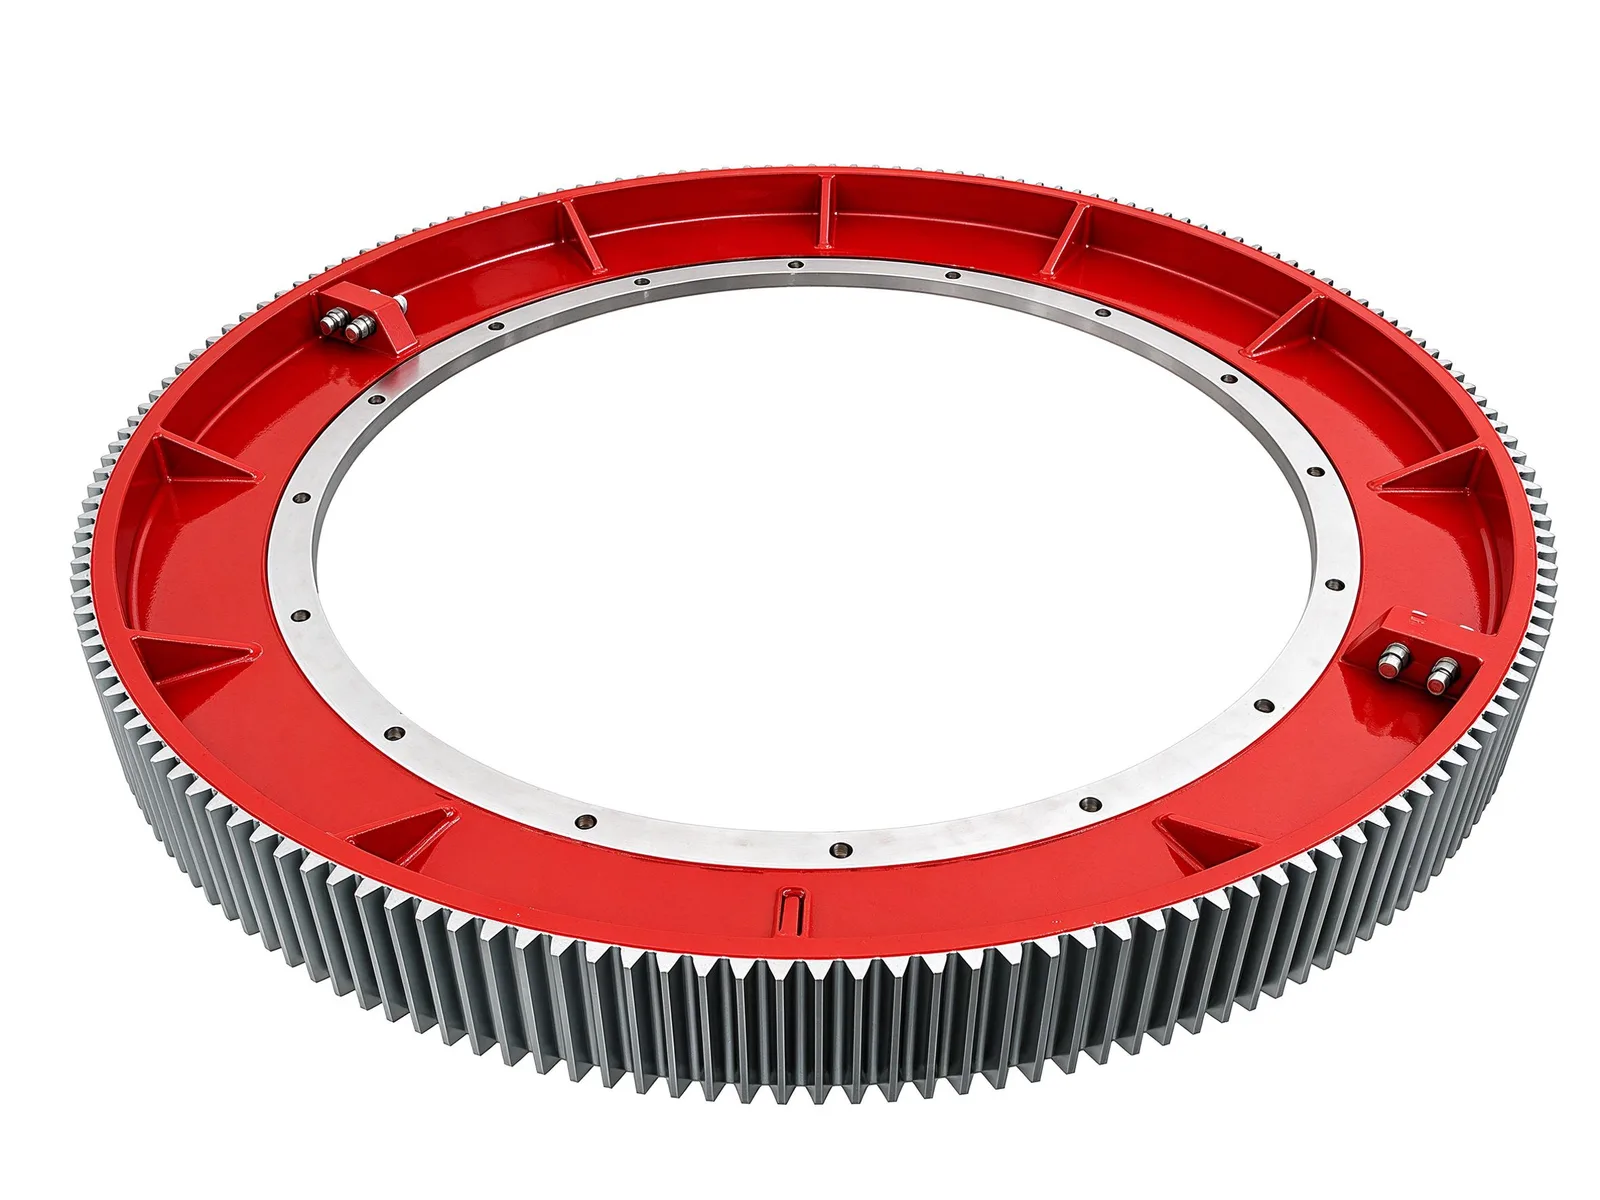
A split-type girth gear with external spur teeth, a ribbed steel web, and an inner bolt flange. It drives rotary kilns, ball mills, and similar heavy-duty drums at low speed and high torque.
Gear Cutting and Heat Treatment
External spur teeth are cut on boring and milling equipment that handles gears up to Ø10 000 mm in outside diameter and module M60. The same shop cuts helical, herringbone, and internal teeth, so the tooth form can follow the drive layout rather than a fixed catalog.
Blanks can be supplied as castings, forgings, or rolled rings in 45#, 42CrMo, or ZG270-500. Quenching and tempering is done in-house, and tooth surfaces can be induction hardened on parts up to Ø10 000 mm to raise wear resistance on the loaded flank.
Split Construction and Field Assembly
Large rings are usually made in two halves that meet at bolted joint lugs, with the joint face machined so the halves align after assembly. An inner flange carries a ring of bolt holes for fastening the gear to the drum end.
Because the ring can be split, it is lifted and installed on site without removing the drum from its bearings. This shortens shutdown work and keeps the replacement within the lifting capacity of a normal plant crane.
Inspection and Quality Control
Tooth pitch, runout, and hardness are checked on every gear before shipment, and ultrasonic testing is available for cast or forged blanks where the drawing calls for it. Dimensional and form reports are issued with the part so the customer can match the gear to the mating pinion.
The tooth profile, lead, and backlash are inspected against the drawing, and the bolt hole pattern on the inner flange is checked against the mating drum flange dimensions.
Customization and Ordering
Each girth gear is made to order from a drawing or a defined set of parameters: outside diameter, module, number of teeth, face width, accuracy grade, tooth hardness, joint type, and bolt hole pattern. Tell us the drum diameter and drive power and we will confirm the tooth geometry.
Typical lead time is within 90 days. Please send the drawing or the missing parameters, and we will quote the ring, the joint hardware, and the machining scope.
Specifications
- Max. outside diameter
- Ø10 000 mm
- Max. module
- M60
- Typical materials
- 45#, 42CrMo, ZG270-500
- Heat treatment
- Quenching and tempering, tooth-surface induction hardening
- Typical lead time
- Within 90 days
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part