Other OEM PartsAssemblies
Vertical Shaft Impact Crusher Wear Cylinder Assembly
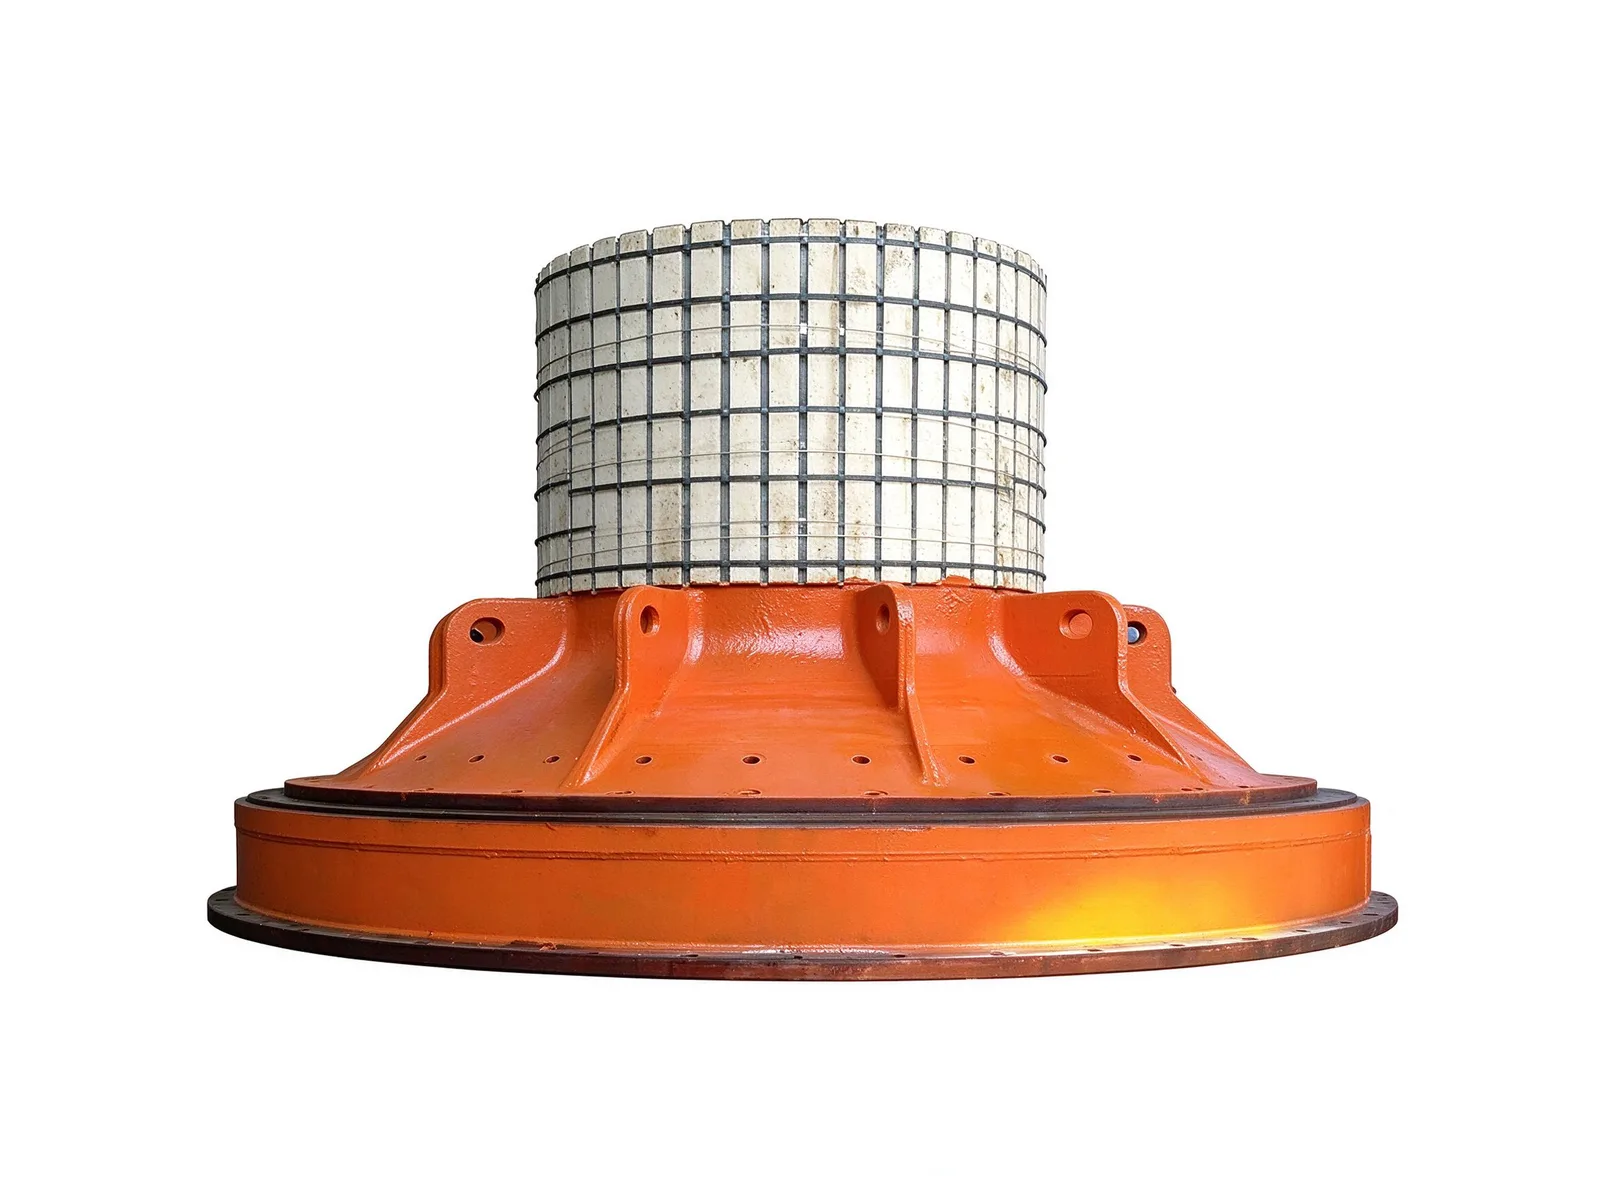
A replaceable wear cylinder assembly for vertical shaft impact crushers, combining a ribbed cast steel flange base with a reinforced cylindrical wear liner to protect the crusher body.
Structure and wear protection
Each unit consists of a cast steel mounting base with radial reinforcing ribs and a cylindrical wear drum. The flange face carries evenly distributed bolt holes for locating and fastening the assembly to the crusher frame.
The drum is built around a steel grid skeleton that anchors the hard wear layer. This reinforced liner absorbs impact and sliding abrasion from the feed, while the tapered transition between flange and drum helps guide material into the crushing chamber with less localized wear at the inlet.
Materials and service conditions
The base is cast as one piece and normalized and tempered to develop strength and toughness under cyclic impact. The wear layer can be supplied in high-manganese steel, high-chromium cast iron, or ceramic composite, selected to balance impact toughness and hardness for abrasive, high-impact feed.
It is used in vertical shaft impact crushers and vertical compound crushers for manufactured sand, aggregate production, ore fine crushing, construction waste recycling, and metallurgical slag processing.
Machining and customization
Flange faces, bolt-hole patterns, mating diameters, and drum interfaces are machined to drawing so the assembly seats correctly on the crusher and can be replaced without reworking the frame.
Custom options include base and drum dimensions, bolt-hole layout, wear-layer material, and liner thickness. Replacement wear cylinders can be supplied separately to reduce downtime and keep the main crusher body in service.
Quality control and inspection
Material certificates are retained for the cast base and wear-layer materials. Heat treatment is recorded, and the finished assembly is checked for flange flatness, bolt-hole position, drum fit, and surface condition before shipment.
Additional inspection requirements such as dimensional reports and material verification can be agreed at order.
Specifications
- Base material
- Cast steel
- Wear layer options
- High-manganese steel, high-chromium cast iron, or ceramic composite
- Heat treatment
- Normalizing and tempering
- Mounting
- Flanged base with evenly distributed bolt holes
- Wear part replacement
- Cylinder can be replaced separately
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- Lead time is set in the quotation and depends on material, size, quantity and inspection scope. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part