Castings & ForgingsSteel castings
Integral Cast Crusher Tooth Roll Sleeve
One-piece cast tooth roll sleeve for toothed roll crushers, with staggered wedge teeth that grip and split coarse feed. The bore is machined for shrink-fit or keyed mounting.
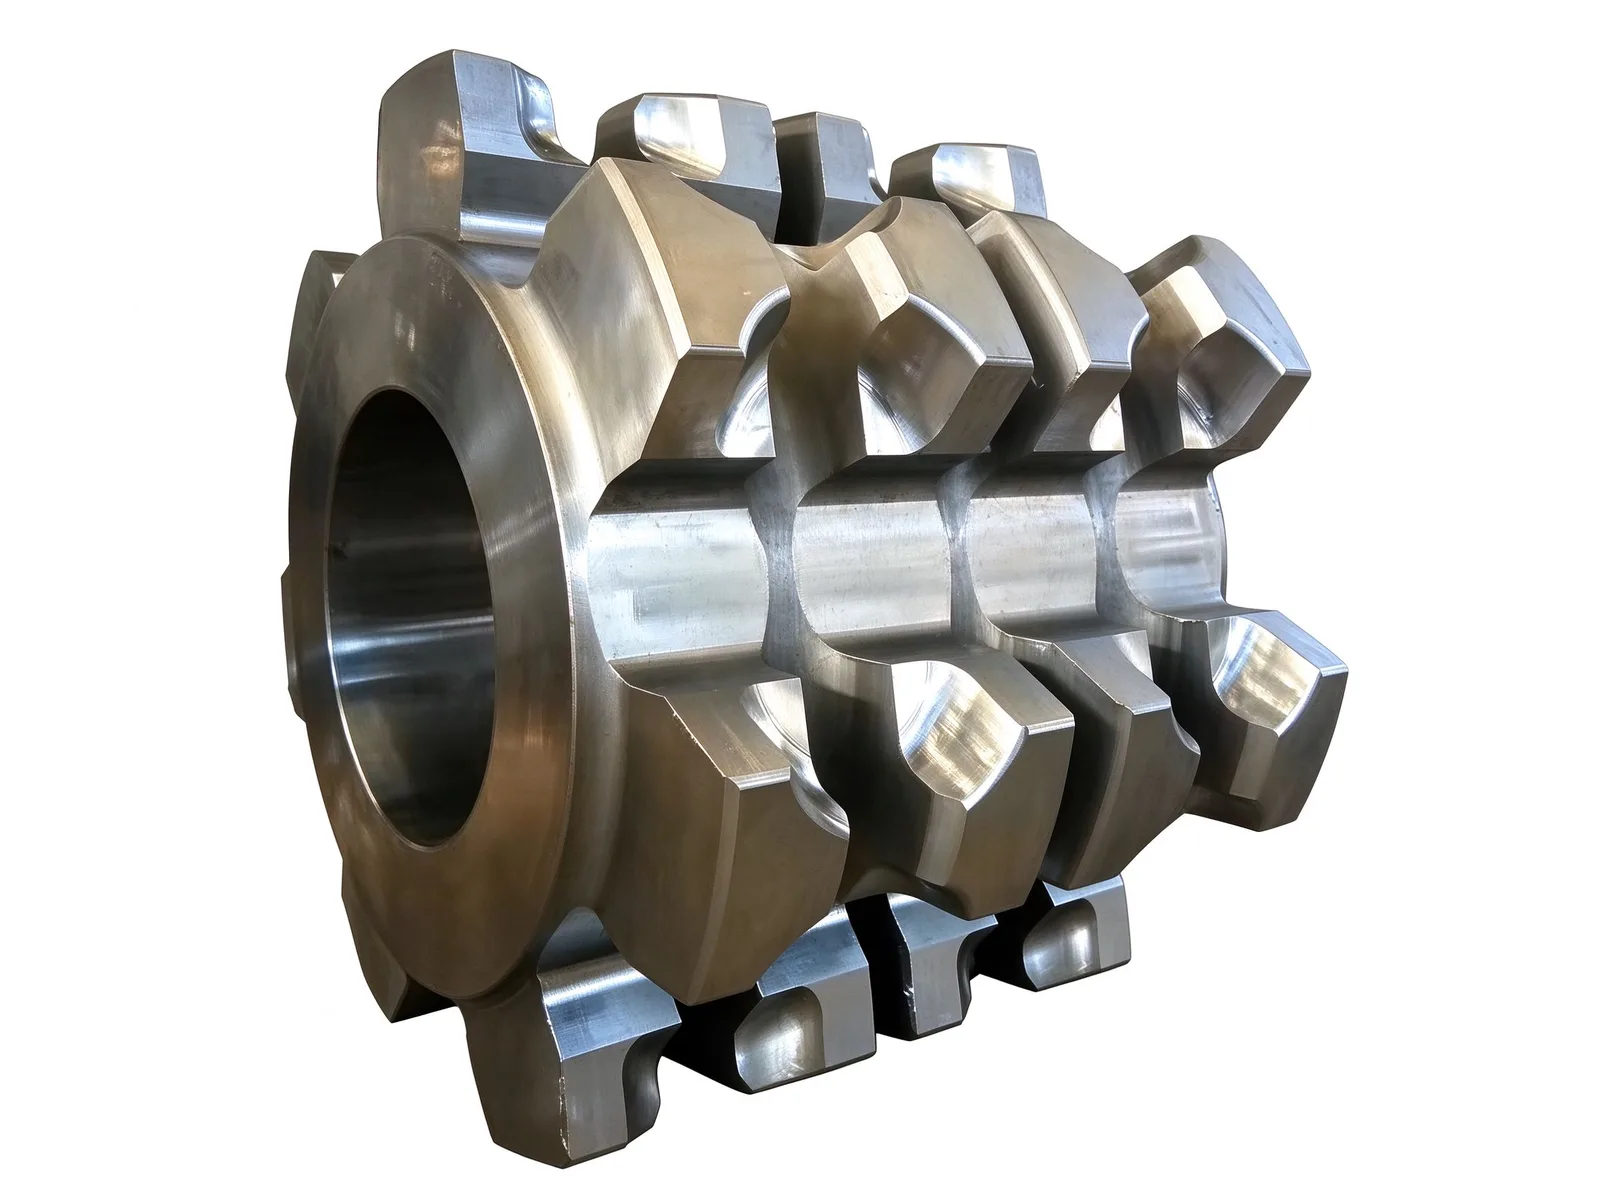
One-piece cast tooth structure
The sleeve is poured as a single casting, so the teeth and the body share one continuous structure with no welded joints. Multiple staggered rows of wedge-shaped teeth run around the outside diameter; each tooth presents a narrow leading edge that bites into the feed and a widening body that splits it.
Because there is no weld seam or assembled tooth, the part takes the direct impact of large lumps without tooth loss or cracking at the tooth root, which is the usual failure point on built-up rolls.
Wear resistance and heat treatment
The sleeve is cast in high manganese steel, high-chrome cast iron or multi-alloy wear-resistant cast steel, then normalized, tempered and water toughened. The heat treatment balances core impact toughness against working-face hardness.
Under impact load the working face work-hardens in service, so surface hardness rises with running hours. This gives a longer service life than plain carbon steel parts in the same duty.
Bore fit and replacement
The central bore is machined as a fit surface and is mounted on the crusher main shaft by shrink fit or by a keyed connection, so torque transfer and running concentricity stay reliable. The staggered tooth rows distribute wear across the full face and even out the load on the material bed.
The sleeve is a replaceable wear part: when the teeth are worn out the whole sleeve is swapped, which protects the main shaft and lowers long-term maintenance cost.
Casting and machining scope
Castings are produced and machined in-house for workpieces up to 8 000 × 4 000 mm and single-piece weights up to 20 t. Stress relief is an in-house process, and dimensional, form and UT/MT inspection are carried out to drawing requirements.
Tooth profile, number of rows, bore diameter and fit, and the mounting method are made to the customer's drawing or the crusher model. Typical lead time is 8–12 weeks.
Specifications
- Material options
- High manganese steel, high-chrome cast iron, multi-alloy wear-resistant cast steel
- Heat treatment
- Normalizing, tempering, water toughening
- Structure
- One-piece cast, no welded joints
- Tooth arrangement
- Multiple staggered rows of wedge-shaped teeth
- Shaft mounting
- Machined bore, shrink fit or keyed connection
Common questions
- Can you machine this part to my drawing?
- Yes. Every part is quoted from the drawing. Send a PDF, DWG, DXF, STEP or IGES file with the material, quantity and any inspection requirements, and we reply within one working day.
- How are the material and heat treatment decided?
- They follow your drawing. The specification table shows the range normally used for this part type; the final material and heat treatment are confirmed with the quotation.
- What lead time and inspection come with the part?
- A single part from the approved drawing usually takes 8–12 weeks; the exact date depends on material, size, quantity and inspection scope and is set in the quotation. Material verification, in-process checks and final inspection records are archived with the part, and any extra certification is agreed before production.
- How is the part packed for export?
- Export parts are rust-proofed and packed for the transport method and destination confirmed in the quotation, with lifting points and markings agreed before dispatch.
Every part is quoted from the drawing itself, not from a size band. Send it over and we answer with the process, the lead time and the tolerance we can hold.
Quote this part